


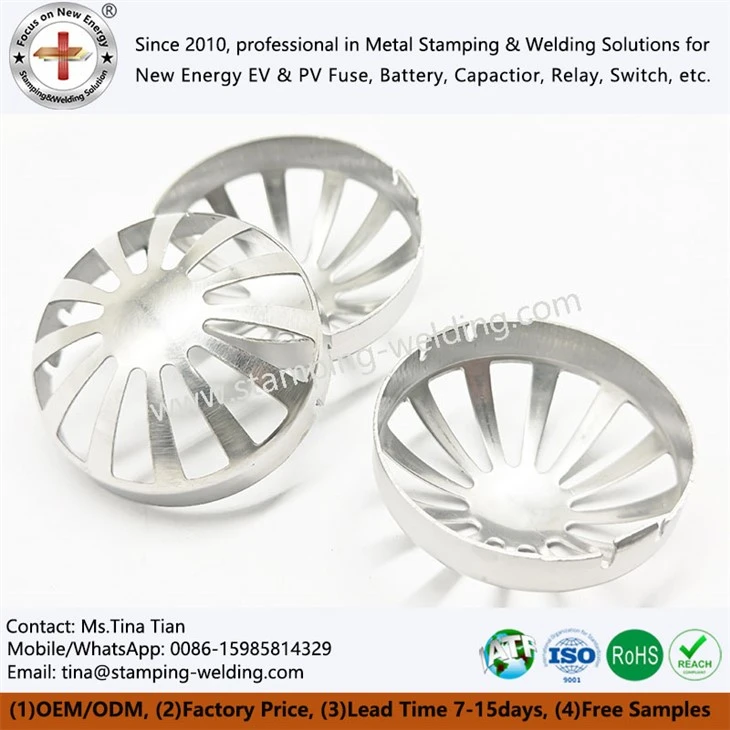
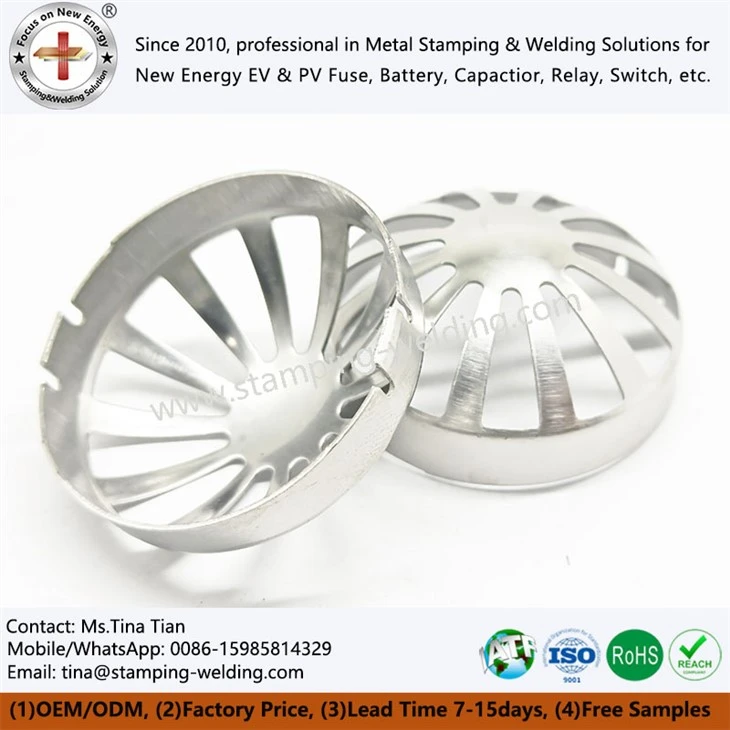
Deep Draw Stamping Components
Deep Draw Stamping Components are designed for filtration assemblies using SUS304 filter caps with controlled geometry and corrosion resistance. Deep drawing, precision punching, final sizing, and inspection meet drawing requirements. Xiamen Apollo provides in-house stamping, deep-drawing tooling, and CNC machining for OEM prototype and volume production, with existing-process samples in 1–2 days and new-tool samples in 20–30 days.
- Fast Delievery
- Quality Assurance
- 24/7 Customer Service
Product Introduction
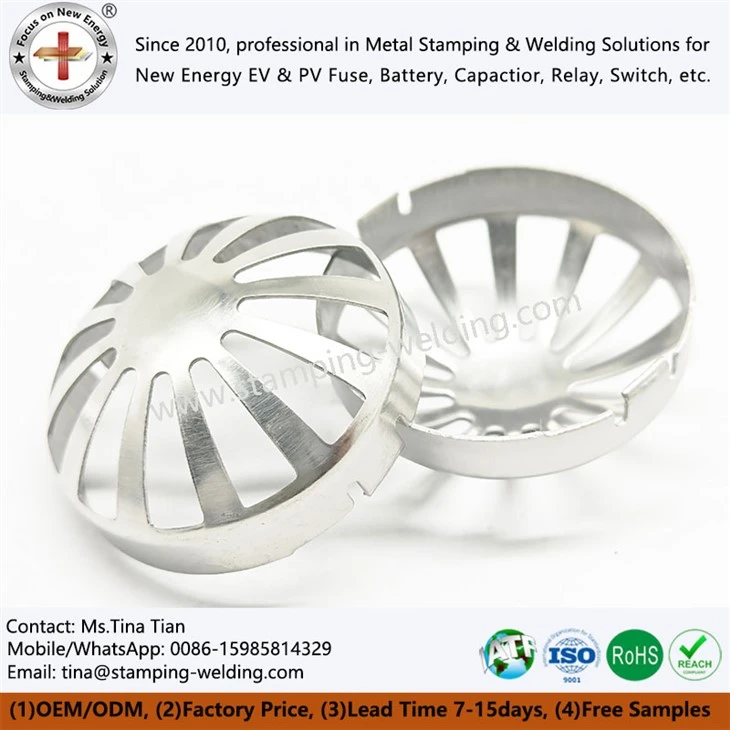
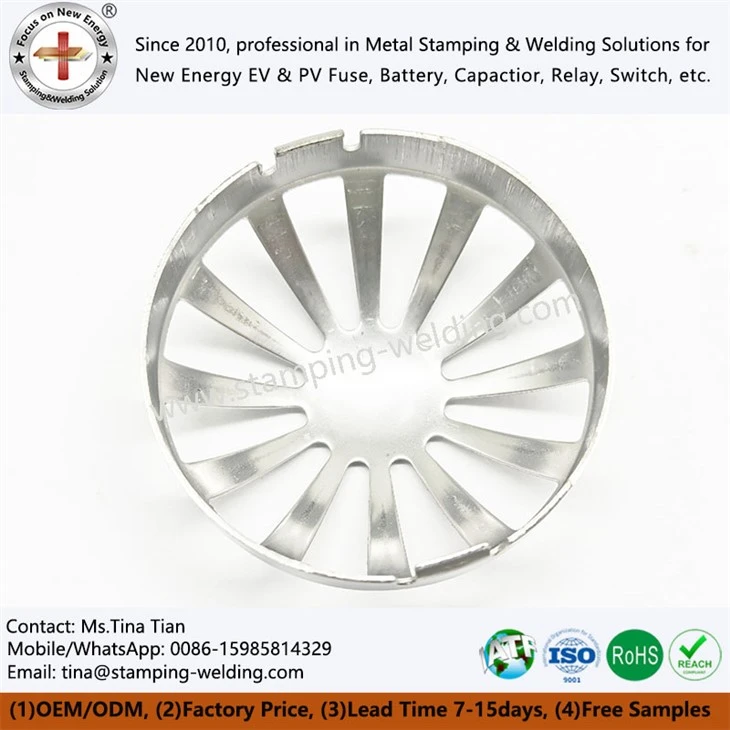
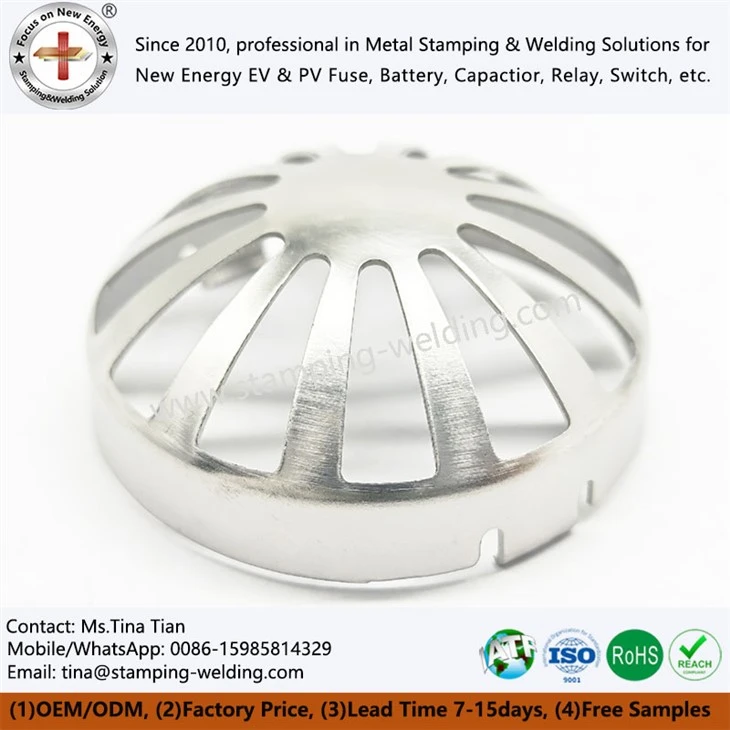
Deep Draw Stamping Components are formed from SUS304 stainless steel sheet into filter caps with controlled cylindrical or rounded profiles, openings, and mating dimensions defined for the filtration assembly. Deep drawing and precision stamping form the component as an integrated piece, maintaining the relationship between the body, end profile, and functional interface while reducing the need for separate component assembly.

Material Advantages of Deep Draw Stamping Components
Corrosion Resistance
SUS304 provides corrosion resistance for filter caps exposed to moisture, process fluids, and common industrial environments. Its surface is suitable for filtration components where the natural stainless steel finish is required for Deep Drawn Metal Stamping.
Deep Drawing Formability
SUS304 stainless steel sheet supports deep drawing into cylindrical and rounded filter-cap geometries. Proper sheet thickness, punch radius, die radius, and forming conditions help control wrinkles, tearing, and dimensional variation.
Surface & Structural Stability
The natural SUS304 surface provides a clean metallic finish without additional coating. Its mechanical properties support formed cap structures, while controlled material selection helps maintain dimensional stability during stamping and assembly.

Manufacturing process of Deep Draw Stamping Components
SUS304 Sheet Preparation: SUS304 stainless steel sheet is inspected for material grade, thickness, surface condition, and flatness before forming. Sheet quality is controlled to support consistent deep drawing and a clean natural finish for Stamping 304 Stainless Steel.
Deep Drawing Forming: The flat SUS304 blank is formed into the filter-cap body through controlled deep drawing. Punch radius, die radius, blank-holder pressure, and forming sequence are adjusted to control material flow and reduce wrinkling or tearing.
Precision Punching & Profile Forming: Required openings, holes, or edge profiles are produced through precision punching after the main drawing operation. Tool clearance and punch condition are controlled to limit burrs and maintain dimensional accuracy for Stainless Steel Stamping Parts.
Final Sizing & Surface Inspection: The formed filter cap is calibrated to the specified diameter, height, rounded profile, and mating dimensions. Final inspection checks critical geometry and the natural SUS304 surface for scratches, dents, and forming defects for Stainless Steel Sheet Metal Stamping.

OEM Customization of Deep Draw Stamping Components
Custom filter caps are developed from 2D drawings, 3D CAD files, or physical samples, with diameter, forming depth, openings, wall profile, and mating dimensions defined according to the filtration assembly. The design is reviewed for SUS304 forming feasibility and final installation requirements for Stainless Steel Stamping Parts.
Tooling is designed around SUS304 sheet thickness, drawing depth, punch radius, die radius, blank-holder conditions, and material flow. The forming sequence is optimized to control wall deformation, rounded geometry, wrinkling, tearing, and dimensional variation during Precision Metal Stamping production.
Initial samples are produced to verify cap diameter, height, forming profile, openings, and assembly fit. Dimensional and surface inspections identify forming deviations, while tooling conditions can be adjusted before the component enters volume Custom Stainless Steel Stamping production.
Validated filter caps move into controlled production using deep drawing, precision punching, sizing, and final inspection. Production parameters are monitored to maintain consistent geometry and natural SUS304 surface condition across batches, with process requirements aligned to the approved customer drawing.

Frequently Asked Questions about Deep Draw Stamping Components
Q: Why is SUS304 used for Deep Draw Stamping Components?
A: SUS304 provides corrosion resistance and suitable forming behavior for filter caps exposed to moisture, process fluids, and industrial environments. Its natural stainless steel surface also avoids the need for an additional decorative coating where the application requires a clean metallic finish.
Q: What should be checked before deep drawing the filter cap?
A: SUS304 grade, sheet thickness, surface condition, and flatness should be verified before forming. Incoming sheet quality directly affects material flow, surface appearance, dimensional consistency, and the risk of wrinkles or tearing during deep drawing.
Q: How are wrinkles and tearing controlled during Deep Drawn Metal Stamping?
A: The forming process is controlled through punch and die radii, blank-holder pressure, lubrication, drawing depth, and forming sequence. These parameters regulate SUS304 material flow and help reduce excessive deformation, wrinkles, tearing, and dimensional deviation.
Q: How is the final Stainless Steel Stamping filter-cap geometry inspected?
A: Final sizing and inspection check the specified diameter, height, rounded profile, openings, and mating dimensions. The natural SUS304 surface is also inspected for scratches, dents, forming marks, and other visible defects that could affect assembly.
Q: Can the filter cap be customized for different filtration assemblies?
A: Yes. Diameter, forming depth, openings, wall profile, rounded geometry, and mating dimensions can be developed from 2D drawings, 3D CAD files, or physical samples. The design is reviewed according to the filtration assembly and SUS304 forming requirements.

Contact Us
Send your 2D/3D CAD drawing, SUS304 sheet thickness, filter-cap dimensions, forming depth, opening requirements, expected volume, and tolerance specifications for DFM review, tooling assessment, sample planning, and a factory-direct quotation.

Hot Tags: Deep Draw Stamping Components,Deep Drawn Metal Stamping,SUS304 Deep Draw Stamping,SUS304 Filter Cap,Stainless Steel Filter Cap,Stainless Steel Sheet Metal Stamping,Precision Deep Drawing,Precision Metal Stamping,Precision Stainless Steel Punching,Filter Cap Forming,Custom Stainless Steel Stamping,OEM Stainless Steel Stamping Parts,Stainless Steel Stamping Parts,Filter Assembly Components,Deep Draw Stamping Manufacturer


