


Electric Cabinet Manufacturer for Industrial Control and Power Distribution
Xiamen Apollo Stamping Welding Technology manufactures custom electric cabinets and sheet metal enclosures for industrial automation, PLC control, and power distribution applications. Production processes include CNC laser cutting, precision sheet metal bending, metal welding, and surface finishing. Material selection covers cold-rolled steel, galvanized steel, stainless steel, and aluminum according to structural load and installation conditions.
Apollo supports drawing review, DFM assessment, tooling coordination, and cabinet fabrication based on customer specifications. Engineering review covers panel thickness, mounting interfaces, bend geometry, welding positions, door alignment, and cable entry locations. Dimensional inspection and project-specific quality documentation can be arranged before production release and batch delivery.
Request a Factory Direct Quote
Explore Our Electric Cabinet Product Catalog
Browse industrial control cabinets, PLC enclosures, and metal electrical cabinets for power distribution, automation, and equipment integration.
-
![Electrical Cabinet Outdoor]() Add to Inquiry
-
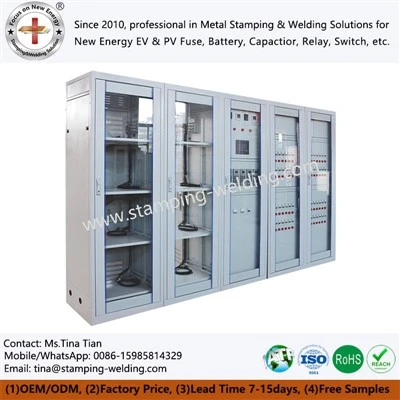
![DC Power Supply Distribution Cabinet]()
DC Power Supply Distribution Cabinet
Add to Inquiry -
![Modular Distribution Cabinets]() Add to Inquiry
-
![DC Distribution Cabinet]() Add to Inquiry
-
![Steel Distribution Cabinets]() Add to Inquiry
-
![Wall-mounted Metal Distribution]()
Wall-mounted Metal Distribution
Add to Inquiry -
![Optical Distribution Cabinet]() Add to Inquiry
-
![Electric Distribution Cabinets]()
Electric Distribution Cabinets
Add to Inquiry -
![Modular Fiber Cabinet]() Add to Inquiry
-
![Odf Cabinet]() Add to Inquiry
-
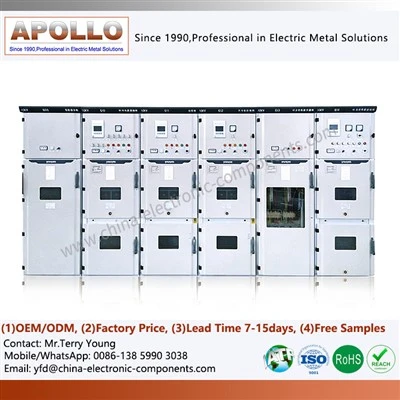
![Metal Electrical Cabinets]() Add to Inquiry
-
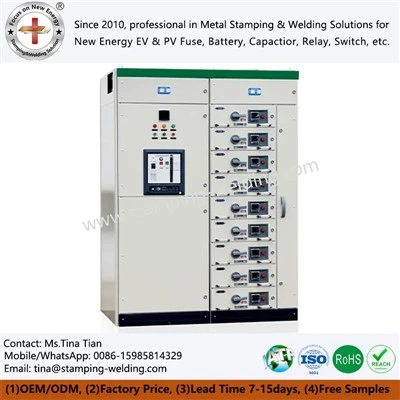
![Low Distribution Cabinet]() Add to Inquiry




Material Standards, Tooling & Forming Processes
Electric cabinet fabrication starts with the equipment envelope, mounting requirements, and operating environment. The material and sheet thickness must provide the required structural stiffness while allowing the cabinet to be formed, welded, coated and assembled without unacceptable distortion.
Cold-rolled steel is commonly used for indoor electrical cabinets and control enclosures where the specified coating system provides the required surface protection. Galvanized steel may be considered where the substrate requires additional corrosion protection. Stainless steel can be specified for applications requiring greater resistance to particular moisture or chemical exposure conditions. Final selection depends on the environment, structural requirements, coating compatibility, and project cost constraints.
Laser cutting is used to produce panel outlines, ventilation openings, cable entries and mounting features. CNC bending forms the cabinet panels, doors, brackets and reinforcing sections. Bend allowance, material thickness, tooling radius and springback must be considered together to maintain the finished dimensions.
Welded frames require control of heat input, joint preparation and welding sequence. Poorly controlled welding can cause door misalignment, panel distortion and inconsistent gasket compression. Where the cabinet uses removable panels or modular assemblies, the manufacturing drawing should also define fastening locations, access clearances, and the interfaces between adjacent sections.
Electric Cabinet Material and Manufacturing Specifications
| Parameter | Engineering considerations | Inspection or verification |
| Cabinet material | Cold-rolled steel, galvanized steel, or stainless steel as specified | Material certificate and grade verification |
| Sheet thickness | Selected according to cabinet size, loading, and panel stiffness | Thickness measurement |
| Panel dimensions | Drawing-defined dimensions and tolerances | Calibrated gauges or optical measurement |
| Mounting features | Hole positions, threaded inserts and equipment interfaces | Dimensional inspection and assembly trial |
| Bending geometry | Bend radius, angle, springback and flange length | Angle gauge and dimensional inspection |
| Welded structure | Joint geometry, weld continuity and distortion limits | Visual inspection and specified weld tests |
| Surface protection | Coating system selected for indoor or outdoor exposure | Coating thickness and adhesion tests as specified |
| Enclosure protection | IP rating defined by the finished enclosure design | Testing to the applicable IEC 60529 requirements |
The values above define the engineering control items. Actual material grades, thicknesses, tolerances, and test acceptance limits should be confirmed in the approved drawing and project specification.
Design for Manufacturability (DFM)
Before releasing a new electric cabinet to production, the following items should be reviewed:
Panel geometry: Confirm that flange lengths, bend radii, and corner clearances are compatible with the forming process.
Mounting interfaces: Verify that rail positions, fixing holes, hinges, and locks match the equipment installation drawing.
Weld access: Check whether the specified joints can be welded and inspected without obstructing adjacent features.
Cable entry: Define gland plate locations, opening sizes and clearance for the intended cable routing.
Service access: Confirm that doors, removable panels and fasteners allow installation and maintenance.
Packaging and transport: Assess panel deformation risk, surface scratching and protection of protruding fittings.
For projects requiring an industrial control enclosure, see our Industrial Electrical Cabinet product range.
Advanced Joining, Insulation & Surface Treatments
The enclosure joining method affects structural stiffness, dimensional stability, appearance and environmental protection. Depending on the cabinet design, manufacturing may use resistance welding, MIG welding, TIG welding, spot welding, or mechanical fastening. The process is selected according to sheet thickness, material type, joint accessibility, and the required load-bearing performance.
Welded frames should be evaluated for joint continuity, distortion, and the condition of the surrounding sheet metal. For doors and panels requiring accurate alignment, the welding sequence and fixture design should control movement before final machining or assembly.
Where the cabinet contains electrical equipment, the design should also identify protective-earth bonding points and the requirements for electrical continuity verification.
Surface Protection and Outdoor Enclosure Design
Powder coating can provide a durable surface finish when the pretreatment, coating formulation, curing conditions, and substrate preparation are properly controlled. Galvanized or stainless steel may be selected for specific exposure conditions, but neither material choice nor coating appearance alone establishes the finished cabinet's corrosion resistance.
For outdoor electric cabinets, the design should address:
Door gaskets and their compression at the closed position.
Cable glands, connectors and other penetrations through the enclosure.
Drainage and condensation management.
Ventilation openings and any associated protective components.
Coating thickness, adhesion and resistance to the specified environment.
Corrosion protection around cut edges, welded joints and fastener interfaces.
IP65 and IP66 are enclosure protection classifications, not generic properties of a sheet metal cabinet. The complete assembled enclosure must meet the relevant ingress protection test requirements in its final configuration, including the applicable doors, seals, cable entries, and ventilation accessories.
Process Selection by Cabinet Type
| Cabinet type | Main fabrication considerations | Project verification |
| Industrial control cabinet | Mounting plates, component access and cable routing | Dimensional and assembly inspection |
| PLC control cabinet | DIN rail mounting, cable separation, and service access | Layout and interface verification |
| Outdoor electric cabinet | Door seals, cable entries and surface corrosion protection | Specified IP and environmental tests |
| Power distribution cabinet | Structural support, equipment clearance and grounding interfaces | Assembly and electrical safety checks |
| Server cabinet | Equipment mounting, cable management and airflow openings | Dimensional and load testing as specified |
| Energy storage cabinet | Structural layout, thermal management and safety-system interfaces | Project-specific structural and environmental validation |
For server and data equipment applications, review the Server Cabinet and Server Enclosure range.
Request Custom Technical Evaluation
Quality Control & Certifications at Apollo
Quality control for an electric cabinet should cover the full manufacturing sequence, from incoming sheet material to the finished enclosure. Inspection criteria should be linked to the approved drawing, bill of materials, surface treatment specification, and required electrical or environmental tests.
Incoming inspection can verify material grade, sheet thickness, and surface condition. During fabrication, checks should focus on panel dimensions, bend angles, mounting-hole positions, weld condition, and frame squareness. After finishing, the inspection plan should address coating appearance, specified coating thickness, door alignment, fastener fit, and any damage around formed or welded edges.
For cabinets designed for outdoor service, IP testing should be performed on the relevant assembled configuration against the specified ingress protection rating. Coating adhesion and corrosion tests should follow the agreed test method and exposure duration. Where required, electrical checks may include protective-earth continuity, insulation resistance, and dielectric withstand testing under the applicable product requirements.
Apollo's manufacturing quality documentation should identify the applicable quality management certifications and their scope. Where a customer program requires PPAP Level 3, the submission package can be defined around the customer's requirements, including process flow, PFMEA, control plan, material records, dimensional results, and process capability data where applicable.
Recommended Inspection Plan
| Inspection stage | Control item | Evidence or record |
| Incoming material | Grade, thickness and surface condition | Material certificate and incoming inspection |
| Laser cutting | Cut dimensions, openings and edge condition | Dimensional inspection |
| CNC bending | Bend angle, flange length and panel geometry | In-process measurement |
| Welding | Joint condition, continuity, and distortion | Weld inspection and specified test results |
| Surface finishing | Coating appearance, thickness and adhesion | Coating inspection report |
| Final assembly | Door alignment, mounting interfaces, and fasteners | Assembly inspection record |
| Electrical verification | Grounding continuity and dielectric tests where required | Electrical test records |
| Environmental qualification | IP rating and corrosion testing where specified | Test report for the relevant configuration |
| Customer quality submission | PPAP or other required quality documents | Approved project-specific submission package |
Traceability and Production Release
For repeat production, the control plan should define how material lots, drawing revisions, tooling changes, and finishing batches are linked to the completed cabinets. Any deviation affecting dimensions, surface protection or assembly interfaces should be reviewed before shipment.
Packaging should protect painted surfaces, door edges, mounting plates and projecting fittings against abrasion and impact during handling. The packaging method, labels, and shipping documentation should follow the customer's delivery requirements.
FAQ
Q: 1. What materials are commonly used for custom electric cabinets?
A: Cold-rolled steel is widely used for indoor control cabinets, while galvanized steel and stainless steel may be selected for specific corrosion conditions. Material selection depends on structural loading, panel dimensions, surface protection, installation environment, and the customer's drawing. The required grade and thickness should be confirmed before tooling and production.
Q: 2. Can Apollo manufacture electric cabinets from customer drawings?
A: Apollo's electric cabinet range includes industrial electrical cabinets, PLC enclosures, and related sheet metal structures. For a custom project, provide 2D drawings or 3D CAD files showing overall dimensions, mounting interfaces, panel thicknesses, door configuration, and cable entries. DFM review can identify forming, welding, and assembly constraints before production release.
Q: 3. Can a custom electric cabinet meet IP65 or IP66 requirements?
A: An IP rating applies to the finished enclosure configuration, not merely to the sheet metal shell. Compliance depends on door seals, cable glands, ventilation openings, fasteners, and assembly quality. The target rating should be agreed before design release and verified through testing to the applicable IEC 60529 requirements.
Q: 4. How are cabinet dimensions and door alignment controlled during production?
A: Dimensional control begins with the approved drawing, datum references, and tolerances for panels, bends, and mounting features. Fixtures and a defined welding sequence help limit distortion. Inspection of frame squareness, hinge positions, door gaps, and gasket compression can identify deviations before final assembly and shipment.
Request a Custom Electric Cabinet Quote
Send Apollo your cabinet drawings and installation requirements for an engineering review before production. The review can address material selection, panel thickness, laser-cut openings, bend geometry, welded joints, door sealing, mounting interfaces, and the inspection scope.
Submit 2D drawings in .DWG or PDF format, 3D CAD models in STEP format, or a specification containing cabinet dimensions, material grade, sheet thickness, surface finish, environmental conditions, and required protection rating.
For projects requiring IP65/IP66 protection, electrical safety verification, or specific corrosion tests, include the applicable standards and acceptance criteria. This allows the manufacturing team to assess the required processes and testing scope before quotation.
Request a preliminary DFM review and factory-direct quotation. A 24-hour response target can be arranged for complete inquiries, subject to drawing complexity and the information provided.
We're well-known as one of the leading electric cabinet manufacturers and suppliers in China. Please feel free to buy high quality electric cabinet at competitive price from our factory. For more information, contact us now.
